Choosing a smart locker or vending machine manufacturer is an important decision for operators, distributors, and solution providers. The equipment must do more than look good in a product catalogue. It needs to work reliably at the deployment site, connect with the required software, support the intended business process, and remain practical to manufacture and maintain as the project grows.
The right supplier should therefore be evaluated as a long-term technology and manufacturing partner. The following capabilities can help B2B buyers compare manufacturers and reduce project risk.
1. Check Whether the Manufacturer Understands Your Industry
A supplier should first understand what the equipment is expected to achieve. Parcel delivery, hot food service, battery swapping, refrigerated retail, temporary storage, and medical supply management all involve different users, safety requirements, workflows, and operating environments.
For example, a hot food vending machine project may require heated or refrigerated storage, controlled pickup, payment integration, remote monitoring, and a layout designed around the operator’s menu and replenishment process. A battery swapping project may require charging control, battery status monitoring, user authentication, and centralized station management.
ZHILAI develops intelligent cabinet solutions across logistics, retail, food service, energy, healthcare, and storage applications. This multi-industry experience helps the company turn an operating requirement into a practical cabinet, electronics, software, and service solution.
2. Evaluate R&D and Customization Capabilities
A reliable manufacturer should be able to manage structural design, industrial design, hardware, embedded control, platform software, and system integration. Buyers should ask which technologies are developed in-house and how the supplier handles custom requirements.
ZHILAI’s development organization covers structural engineering, automation, hardware, software, and pilot production. Customer requirements can be translated into product specifications, system architecture, technical parameters, and verification plans. The company develops core control boards, communication boards, and functional expansion boards, helping hardware and software operate as one system.
Its terminal software supports Windows, Linux, and Android, while its SaaS architecture can connect multiple device types and centralize business data. These capabilities allow ZHILAI to support standard products as well as customized smart locker, vending, and battery swapping cabinet projects.
According to company materials, ZHILAI holds 559 valid patents and 200 software copyrights covering areas such as vending machines, parcel lockers, food pickup cabinets, battery swapping cabinets, and refrigerated cabinets.
3. Ask How Products Are Tested Before Mass Production
Product validation is especially important for equipment that operates outdoors, handles food, charges batteries, or is used continuously. A professional manufacturer should have a clear process for moving from concept to prototype and volume production.
ZHILAI follows a product lifecycle that includes concept development, engineering validation testing (EVT), design validation testing (DVT), production validation testing (PVT), and mass production. Its testing system covers functionality, performance, reliability, electrical safety, environmental adaptability, and durability.
Available evaluations include high- and low-temperature testing, electrostatic discharge, surge immunity, vibration, rain, dust, tilt, anti-pry protection, lock endurance, and battery charge-discharge cycling. Across its product portfolio, ZHILAI has obtained certifications including CCC, CQC, CE, RoHS, VDE, CB, cETLus, FCC, and NSF. Buyers should confirm which certifications apply to their selected configuration and destination market.
4. Confirm Manufacturing Capacity and Delivery Control
A prototype alone does not prove that a supplier can manage repeat orders. Buyers should review factory capacity, production processes, material control, packaging, and international delivery experience.
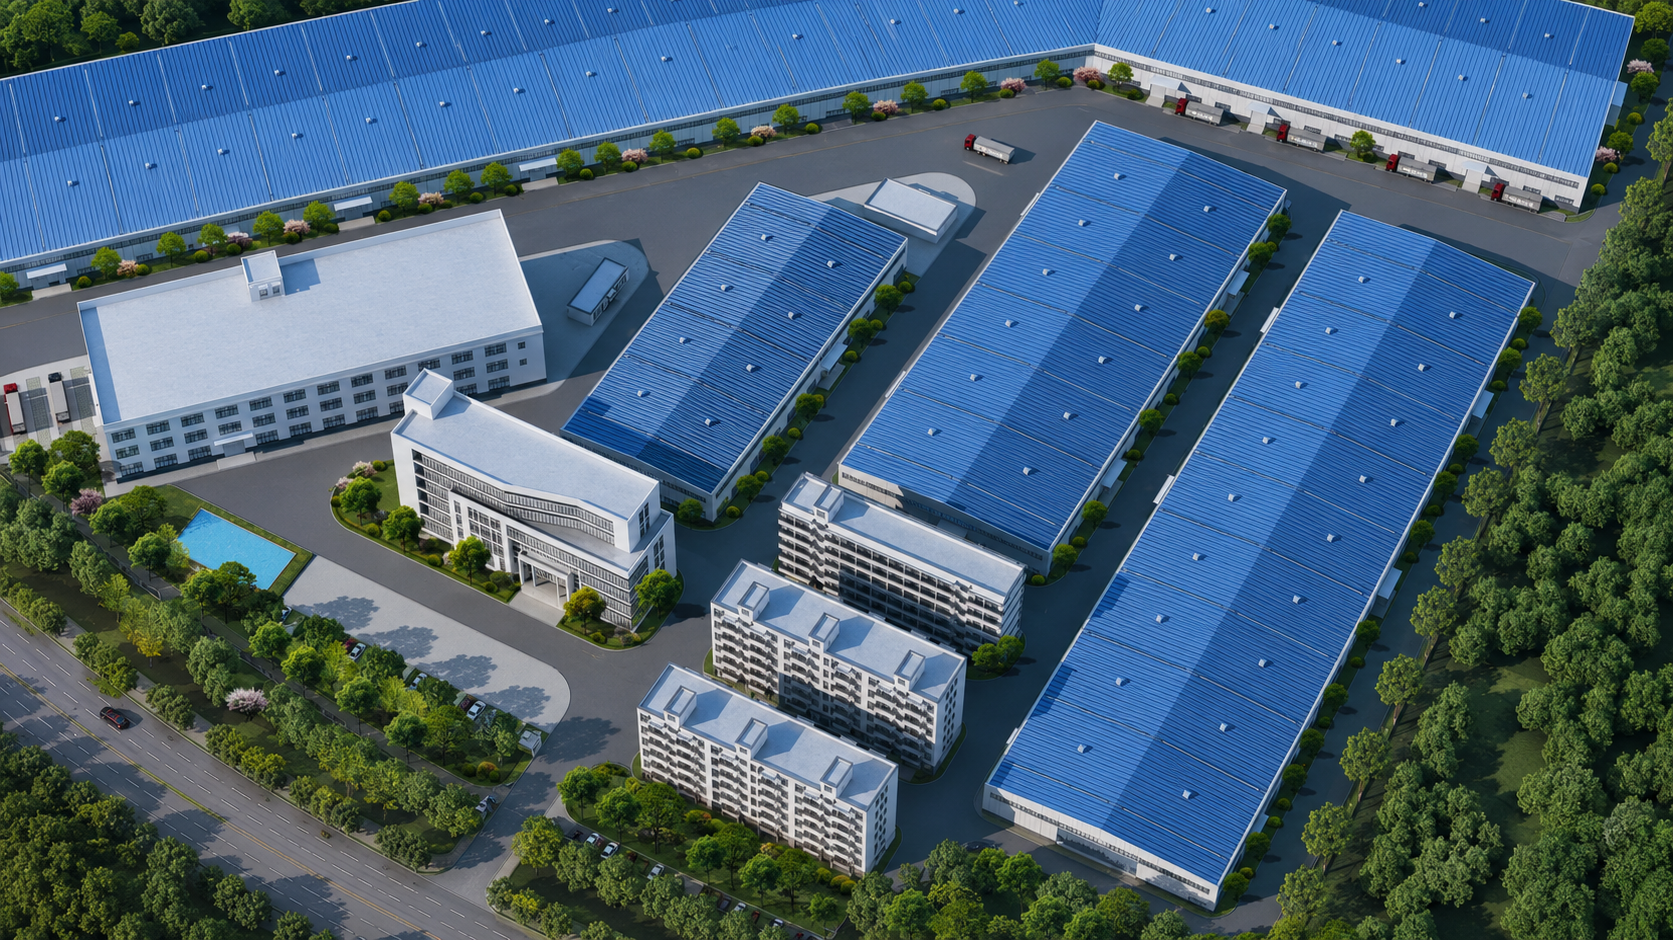
ZHILAI operates manufacturing facilities in Xianning, Hubei, and Vietnam. Company materials state that these facilities total approximately 190,000 square meters and provide annual production capacity exceeding 280,000 units.
Production processes cover sheet-metal fabrication, welding, electrophoresis, powder coating, component assembly, complete cabinet assembly, safety inspection, performance testing, and packaging. This integrated capability supports the transition from samples to volume deployment while maintaining consistent specifications.
5. Review Quality Management and After-Sales Support
Quality control should extend beyond final inspection. A dependable manufacturer needs to manage suppliers, incoming materials, production processes, outgoing inspection, technical changes, and corrective actions.
ZHILAI applies quality management throughout the supply chain and manufacturing process. Its controls include supplier qualification, incoming material inspection, first-article approval, process FMEA, control plans, in-process testing, functional inspection, packaging inspection, and outgoing quality control. PMS, PLM, and ERP systems connect project information, technical documents, purchasing, production, and inventory.
Buyers should also examine documentation, training, spare-parts management, remote technical support, and service response arrangements. These capabilities become increasingly important when equipment is installed across multiple cities or countries.
Conclusion
The best smart locker or vending machine manufacturer is not simply the supplier offering the lowest initial price. Buyers should compare industry knowledge, R&D ownership, validation methods, manufacturing capacity, quality systems, and after-sales support.
ZHILAI combines these capabilities to provide standard and customized solutions for parcel delivery, food pickup, unattended retail, hot meal service, battery swapping, storage, and other intelligent cabinet applications. For B2B customers planning a pilot or a large-scale deployment, this full-process capability can make it easier to move from an initial concept to reliable commercial operation.